Ultrasonic Leaching of Rare Earth Elements from Ashes
Ultrasonic leaching can increase extraction yields and shorten processing times when recovering rare earth elements from ash. By improving contact between ash particles and leaching agents, power ultrasound accelerates dissolution and helps make valuable elements more accessible. Studies on coal fly ash demonstrate the potential: researchers reported 97% yttrium extraction, while a separate study on gallium and vanadium reduced the acid leaching time from 180 to 20 minutes.
Ash as a Secondary Resource for Rare Earth Elements
Ashes represent a promising secondary resource for rare earth elements (REEs). Coal combustion residues can contain yttrium and other rare earths used in electronics, energy technologies and advanced materials. Recovering these elements from existing ash streams and deposits could diversify raw material supplies and turn a disposal material into a useful feedstock.
The extraction potential depends on both elemental concentration and accessibility. An ash may contain valuable elements, yet release only a limited fraction during leaching if the surrounding mineral matrix restricts reagent access. Consequently, ash composition, pretreatment and leaching chemistry must be considered together. Recovering several valuable elements from the same feedstock may also improve the prospects of a process.
Ultrasonic leaching fragments ash particles making rare earths available to leaching reagents. By improving mass transfer between particles and reagent, sonication increases recovery whilst shortening processing time!
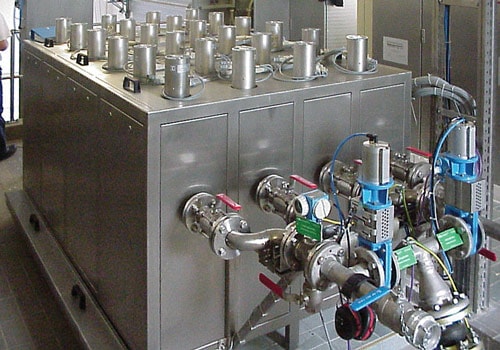
Industrial installation of Hielscher sonicators: 48kW sonicator cluster for the inline leaching of rare earth elements from coal ashes
How Ultrasound Improves Ash Leaching
Power ultrasound intensifies solid–liquid extraction through acoustic cavitation. Microscopic bubbles form and collapse in the liquid, generating local shear forces, microjets and intense mixing. These effects can disperse particle agglomerates, clean exposed surfaces and improve transport of leaching agents to reactive sites. Dissolved species are transported away more rapidly, helping sustain dissolution.
For ash processing, these effects offer several practical advantages:
- Faster leaching: Enhanced mass transfer can shorten the time needed to extract accessible metals.
- Higher extraction yields: Improved surface contact can help release material that remains insufficiently leached under conventional mixing.
- Combination with pretreatment: Ultrasound can intensify the leaching stage after activation has made resistant phases more accessible.
- Flexible process development: Sonication can be developed adapted to varying acid concentration, solids loading, temperature and treatment time.
Research Examples: High Yields and Shorter Leaching Times
The following studies illustrate these advantages under specific experimental conditions. Yttrium is a rare earth element; gallium and vanadium are other valuable metals. Their extraction provides complementary evidence for ultrasonic processing of ash.
Yttrium and Vanadium: Up to 97% and 100% Extraction
Masoum et al. (2021) investigated the extraction of vanadium and yttrium from coal fly ash using sulfuric acid, hydrogen peroxide and ultrasound. The researchers applied response surface methodology to optimize the solid-to-liquid ratio and the proportions of sulfuric acid and hydrogen peroxide. Under the optimized conditions, reported extraction reached 100% for vanadium and 97% for yttrium.
A modified shrinking core model indicated that mass diffusion controlled the reaction rate. This finding highlights the importance of transport processes in the investigated system and supports targeting mass transfer during process optimization. The results demonstrate that high yttrium extraction is achievable with the combined treatment, although the reported yields reflect the complete reagent and ultrasound system.
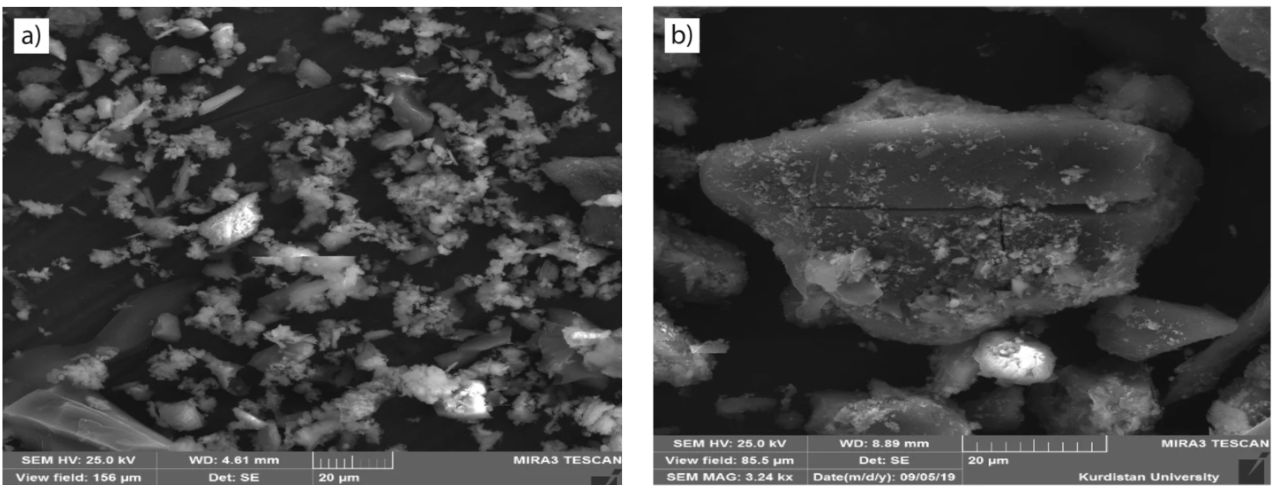
FESEM images of raw coal ash (a) left before leaching coal ash, (b) after ultrasonic leaching.
Study and images: ©Masoum et al., 2021
Gallium and Vanadium: 88.89% Shorter Leaching Time
Zhang et al. (2026) investigated ultrasonic acid leaching following sodium carbonate activation roasting. The optimized pretreatment consisted of roasting at 850°C for 60 minutes, using a fly ash-to-Na₂CO₃ mass ratio of 2:1. Subsequent ultrasonic acid leaching achieved high gallium and vanadium extraction within 20 minutes.
| Parameter | Ultrasonic leaching after activation roasting | Conventional leaching |
|---|---|---|
| Leaching time | 20 min | 180 min |
| Gallium leaching efficiency | 98.14% | 63.81% |
| Vanadium leaching efficiency | 92.32% | 83.56% |
The reduction from 180 to 20 minutes corresponds to an 88.89% shorter leaching stage. Kinetic analysis indicated increased rate constants and enhancement of both mass transfer and interfacial reaction processes. These results demonstrate the potential of combining activation roasting with ultrasonic leaching. The time saving applies to leaching; roasting remains an additional processing step.

Ultrasonically enhanced acid leaching operates at a rate twelve times faster than conventional acid leaching, due to the beneficial mechanical action of cavitation bubbles bursting near the surface. This phenomenon improves acid solution mixing, thereby enhancing transport properties.
Image and study: © Canciani et al., 2024
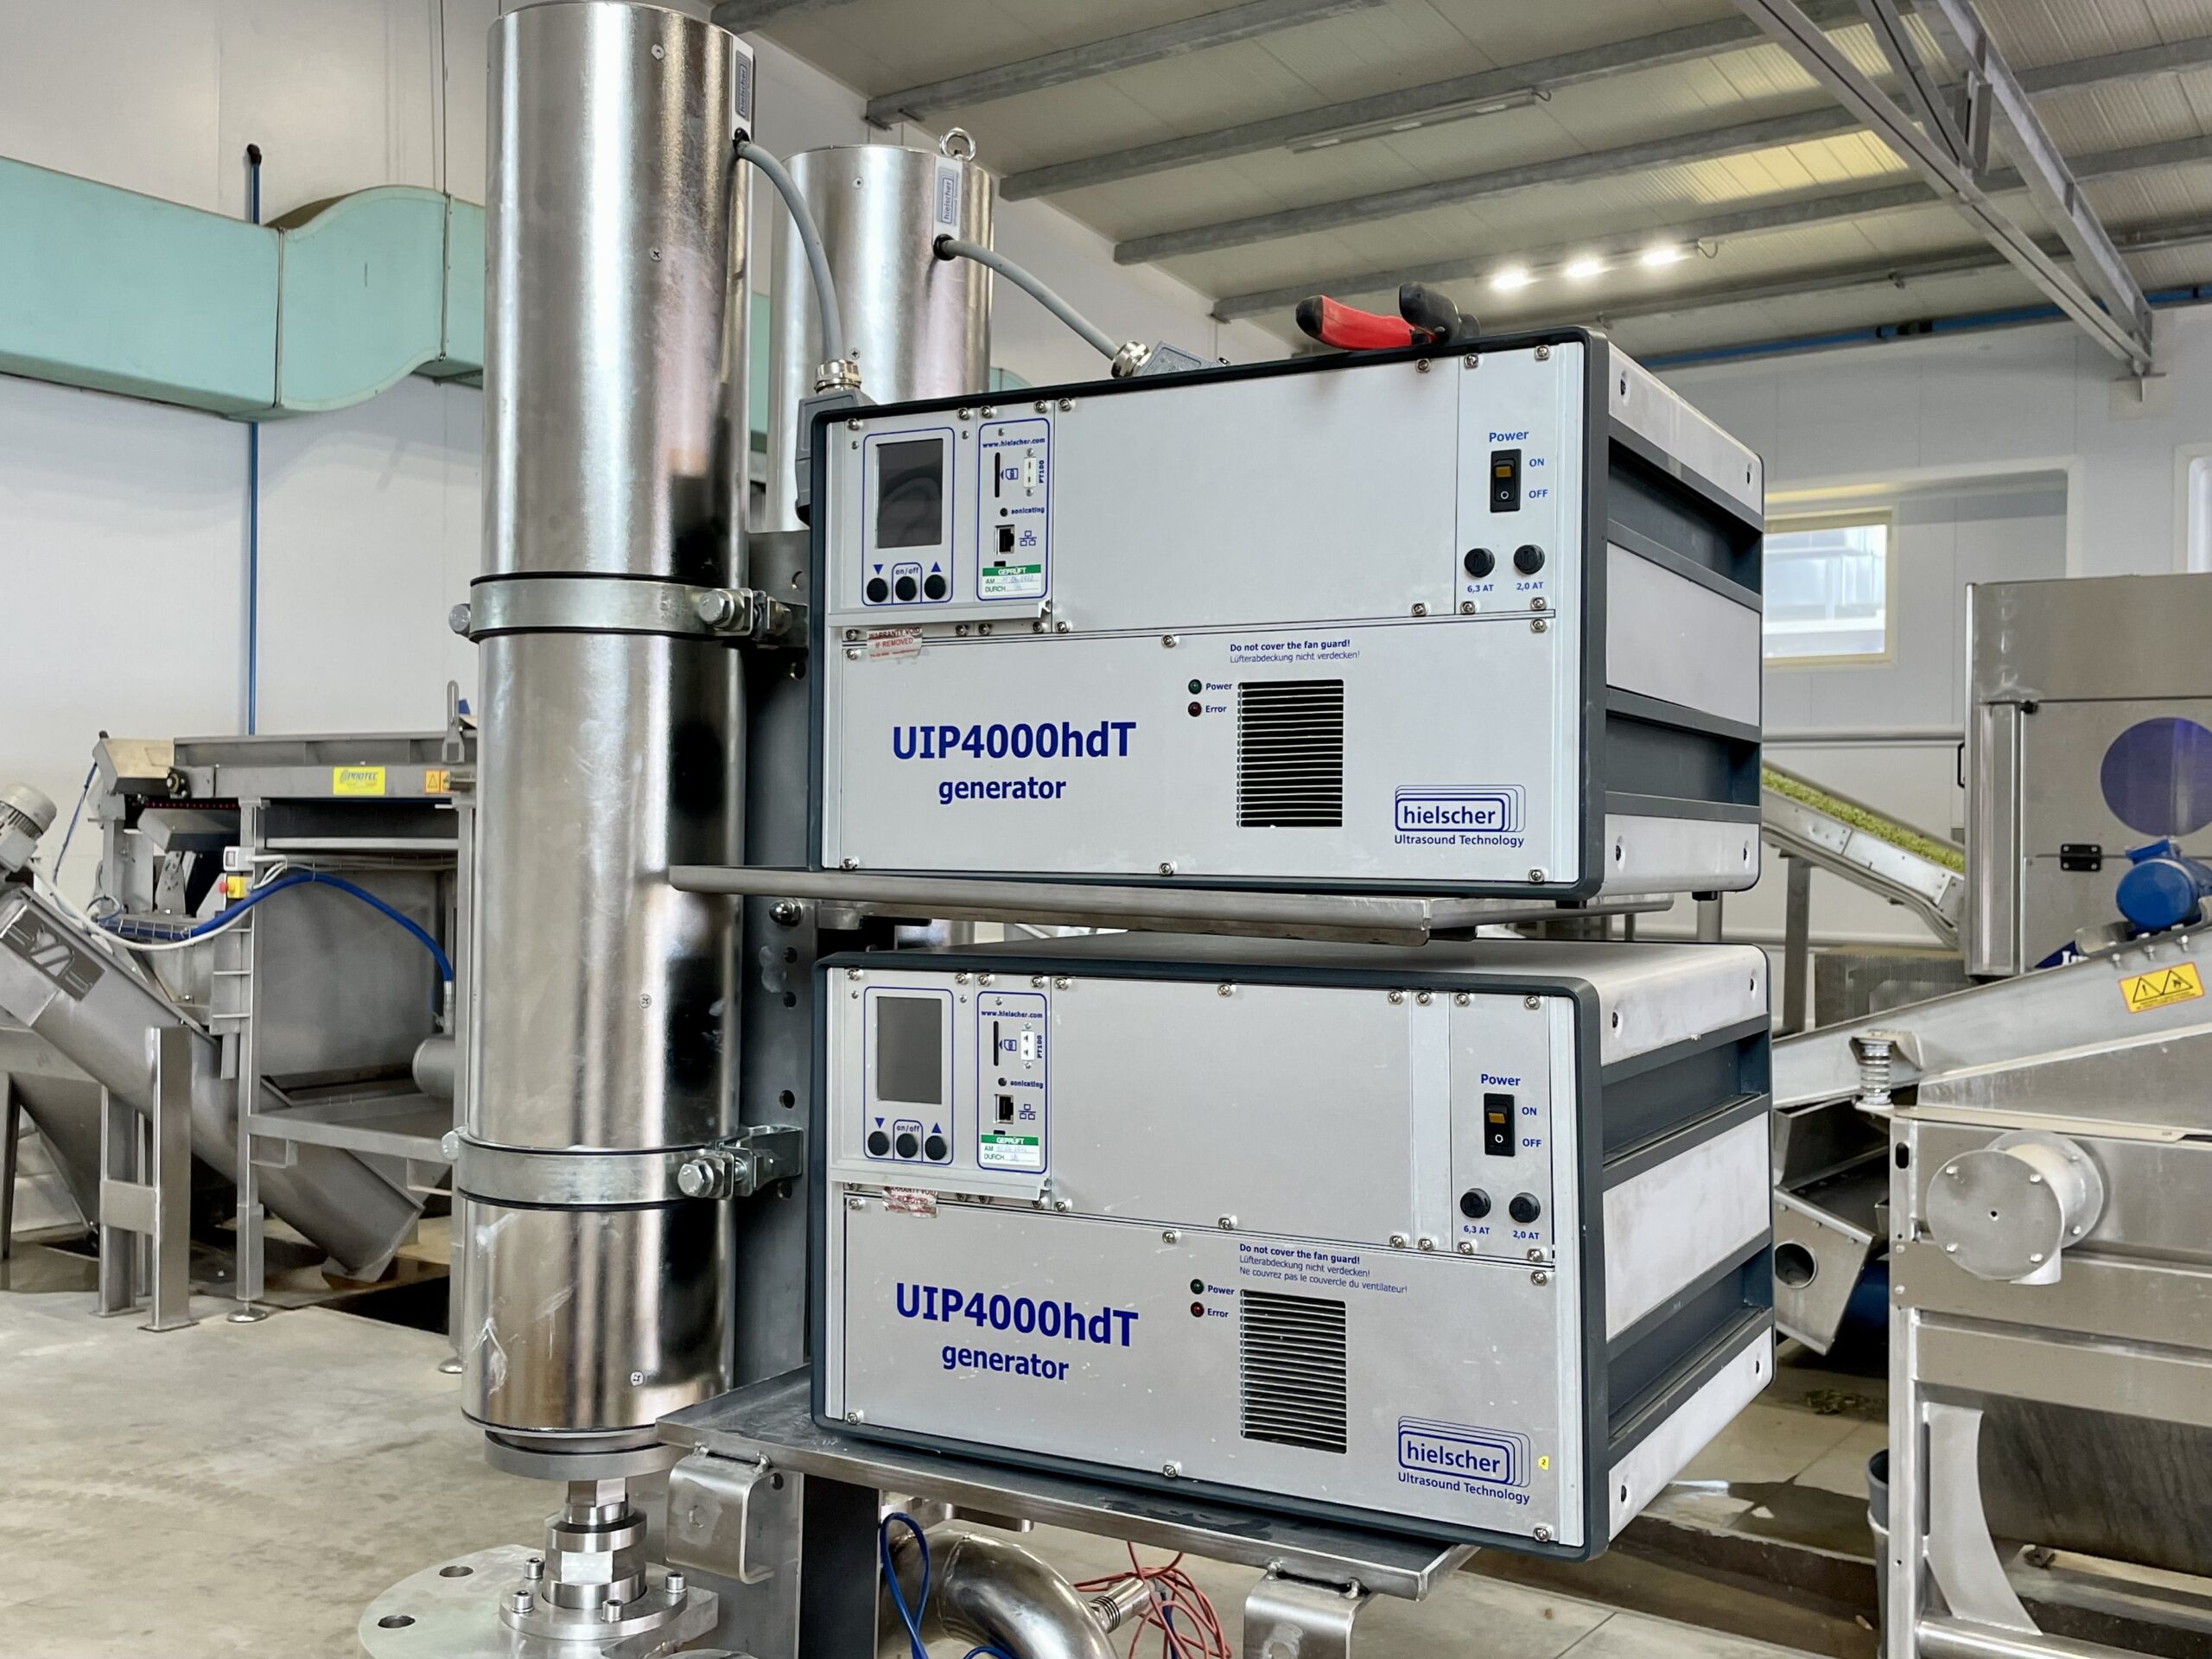
2 industrial sonicators UIP4000hdT for heavy duty processing
Develop your Ultrasonic Leaching Process for High Rare Earth Recovery
For practical rare earth extraction, leaching is followed by separation and purification of the dissolved elements. High leaching efficiency therefore represents an important intermediate result, rather than the yield of a finished rare earth product. Process evaluation should include downstream recovery, reagent use and the energy required for both pretreatment and sonication.
Hielscher offers industrial-grade bench-top sonicators and heavy-duty ultrasonic flow reactors for developing and implementing intensified leaching processes. Equipment selection and trials can establish suitable amplitude, solids loading, residence time and temperature control for a particular ash.
Simple scale-up to large volumes: Once established parameters for optimal recovery can be then linearly scaled-up to any commercial leaching volume.

Hielscher Ultrasonics manufactures high-performance ultrasonic homogenizers for mixing applications, dispersion, emulsification and extraction on lab, pilot and industrial scale.

SEM images for particles at different times of conventional (a–c) and ultrasonic (d–f) leaching.
Image and study: © Canciani et al., 2024
Frequently Asked Questions
How does ultrasound improve rare earth leaching from ash?
Ultrasound generates acoustic cavitation in the leaching slurry. Collapsing bubbles produce intense local mixing, shear forces and microjets that improve contact between ash particles and the leaching solution. These effects expose reactive surfaces and accelerate mass transfer, helping increase extraction yields and shorten leaching times.
What rare earth elements and valuable metals can be leached from ashes?
Depending on their origin and mineral composition, ashes can be leached to extract rare earth elements, including lanthanum (La), cerium (Ce), neodymium (Nd), dysprosium (Dy), yttrium (Y) and scandium (Sc). Coal fly ash is a potential source of these elements.
Other valuable metals include gallium (Ga) and vanadium (V) in suitable coal ashes, and copper (Cu) and zinc (Zn) in municipal waste incineration ashes.
Why use a heavy-duty probe sonicator for ash leaching?
A probe sonicator introduces ultrasonic energy directly into the slurry through a sonotrode (ultrasonic probe/rod). This enables intensive treatment of solid–liquid mixtures and provides adjustable processing conditions. Hielscher industrial sonication equipment supports integration into leaching circuits where controlled energy input and reliable operation are essential. The configuration should match the slurry composition, solids loading and required throughput.
Here are a few of Hielscher leaching applications:
Can Hielscher sonicators operate continuously?
Yes. Hielscher industrial sonicators such as the UIP500hdT (500W) up to UIP16000hdT (16,000W) are designed for continuous 24/7 operation. They can be configured for batch treatment, recirculation or continuous processing through an ultrasonic flow cell. For ash leaching, an installation is integrated into slurry pumping, temperature control and the selected leaching chemistry.
Can ultrasonic leaching be scaled up to industrial production?
Yes, Hielscher sonicators allow a linear scale-up. Hielscher offers equipment for laboratory trials, pilot processing and industrial production, including 16 kW processors that can be combined in clusters. Scale-up starts with trials to establish suitable amplitude, energy input, temperature and residence time. These results provide the basis for selecting reactor capacity and validating extraction performance at the required throughput.
Does ultrasound replace acids or activation roasting?
Ultrasound intensifies the leaching process, while chemical reagents provide the chemistry needed to dissolve the target elements. Some ashes may also require pretreatment to make resistant mineral phases accessible.
Which process parameters can be monitored?
All Hielscher sonicators from 200 watts up support monitoring and automatic recording of amplitude, power, treatment time and temperature, with pressure measurement available through an optional sensor. These data help compare trials and reproduce operating conditions reliably. Rare earth elements extraction efficiency must be determined separately through chemical analysis of the feed, leachate and remaining solids.
Can ultrasonic equipment be used with acidic, abrasive ash slurries?
Hielscher Ultrasonics offers solutions to sonicate acidic, abrasive ash slurries. Sonotrodes, flow cells, seals and other wetted components need to be selected against acid composition, concentration, temperature and particle abrasiveness.
Does higher leaching efficiency mean higher final rare earth recovery?
Yes, higher leaching efficiency means that more of the target element is transferred into the liquid phase. Producing a usable rare earth product also requires downstream separation and purification. Overall recovery depends on the performance of the complete process.
How do I select a Hielscher sonicator for my process?
Start with representative ash samples and define the target elements, slurry concentration, leaching chemistry, batch volume or flow rate, and desired extraction yield. We at Hielscher can help you to select equipment for feasibility trials and subsequent linear scale-up. Our technical center and process laboratory also offers trials to support equipment selection.
Literature / References
- Masoum, H.G., Rastegar, S.O. and Khamforoush, M. (2021): Ultrasound-Assisted Leaching of Vanadium and Yttrium from Coal Ash: Optimization, Kinetic and Thermodynamic Study. Chemical Engineering and Technology 44, 2021. x2249-2256.
- Qian Zhang, Deqing Zhu, Siwei Li, Jian Pan, Zhengqi Guo, Congcong Yang, Jiachen Gong (2026):
Ultrasonic enhanced leaching for the synergistic extraction of Ga and V from fly ash. Journal of Environmental Chemical Engineering, Volume 14, Issue 5, 2026. - Chiara Canciani, Elia Colleoni, Varaha P. Sarvothaman, Paolo Guida, William L. Roberts (2024): On the effect of cavitation on particles in leaching processes: implications to battery recycling. Environmental Advances, Volume 17, 2024.
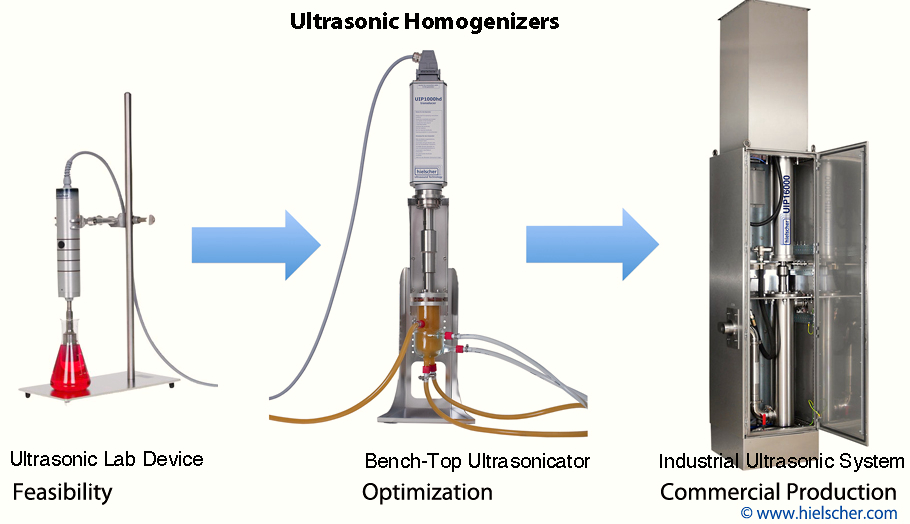
Hielscher Ultrasonics manufactures high-performance ultrasonic homogenizers from lab to industrial size.